Capturing machine cycle times, part counts, and Run/Idle/Stop operating telemetry from CNC machining centers and mechanical stamping punch presses relies on non-invasive industrial IoT engineering: 20G shock-resistant sensor hardening, optical isolation on 24VDC Andon tower lights, M02/M30 cycle completion relays, and spindle motor current profiling to distinguish productive cutting from non-productive air-cuts.
This technical guide is part of DeviceLab's comprehensive engineering handbook on industrial IoT for machinery and equipment.
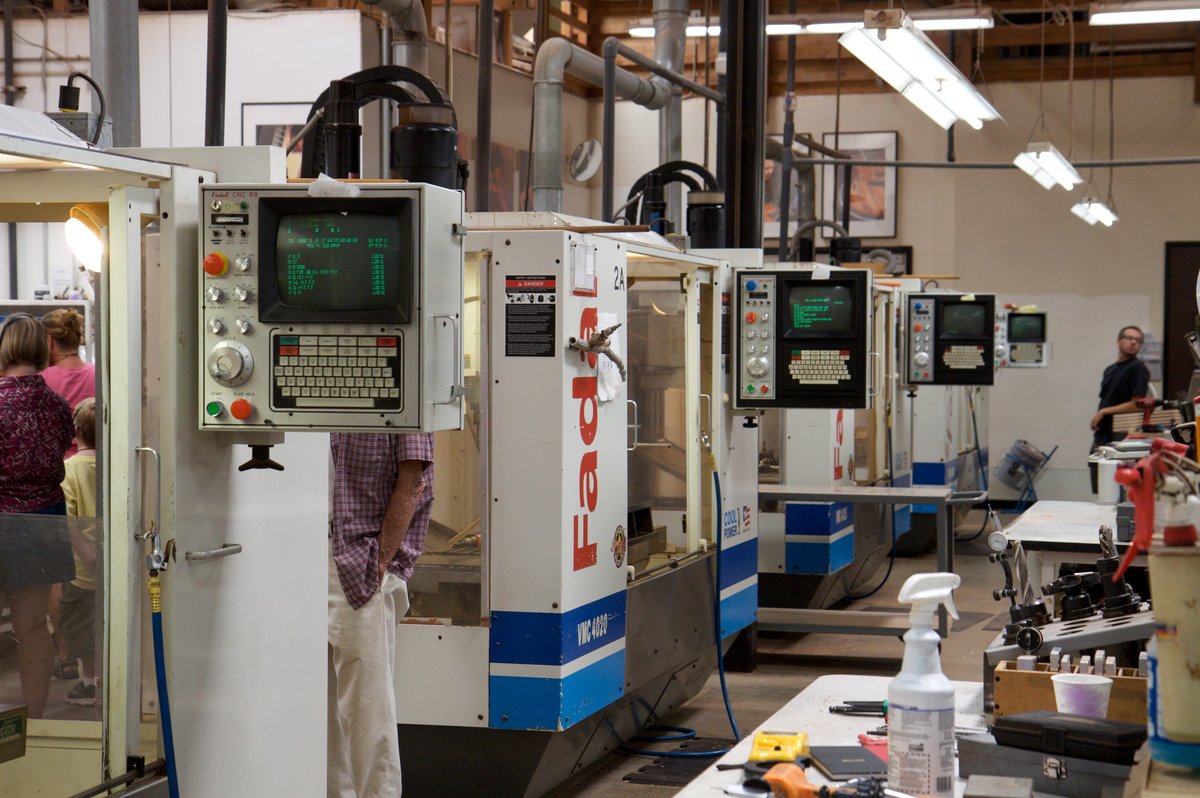
In metalworking, automotive parts fabrication, and precision mold tooling facilities, legacy stamping presses and CNC milling/turning centers (Fanuc, Mazak, Doosan, Komatsu, Aida) frequently lack Ethernet connectivity or operate under proprietary CNC controller software. Production managers struggle with inaccurate shift reporting, undetected machine micro-stops, and excessive tool wear caused by improper feed rates. Non-invasive edge telemetry resolves these operational blind spots without touching CNC controller software.
Electromechanical Matrix: Mechanical Stamping Presses vs. CNC Machining Centers
Designing telemetry hardware for precision machine shops requires understanding the stark electromechanical differences between high-impact punch presses and high-speed CNC tools:
| Operational & Electromechanical Metric | Mechanical Stamping Punch Press (e.g. Komatsu, Aida) | CNC Machining Center (e.g. Fanuc, Mazak, Doosan) | Telemetry Engineering Design Requirements |
|---|---|---|---|
| Mechanical Vibration & Shock Profile | Extreme repetitive impact shock reaching 15G to 25G on flywheel stroke. | Smooth rotational dynamics; continuous high-frequency vibration (<2G). | Presses require silicone-potted electronics, M12 screw connectors, and damping rubber mounts. |
| Cycle Duration & Dynamics | Ultra-fast discrete strokes: 0.8s to 3.0s per stamped part. | Complex multi-step machining cycles: 2 minutes to 45 minutes per part. | Presses require microsecond hardware interrupts; CNCs require continuous spindle load integration. |
| Primary Downtime Causes | Die coil jam, slug pull-up, manual coil strip feeding, raw strip runout. | Tool breakage, part clamping/setup, chip buildup, waiting CNC program upload. | Firmware state machines must track distinct operator reason codes at the machine terminal. |
| Electrical Noise & Transient Spikes | Massive inductive voltage kicks from large pneumatic clutch/brake solenoid coils. | High-frequency harmonic noise generated by 15kW–30kW servo spindle VFDs. | Presses require bidirectional TVS surge suppression; CNCs require high-frequency optical isolation. |
| Cycle Signal Extraction Points | Crankshaft inductive proximity sensor, rotary cam limit switch, clutch valve tap. | 3-color 24VDC Andon light, M02/M30 relay output, spindle motor current transformer. | Non-invasive wiring topologies must prevent false double-counting caused by mechanical chatter. |
20G Shock-Resistant Hardware Hardening for Mechanical Punch Presses
Standard electronic enclosures and plastic screw terminals rapidly fail when mounted directly on heavy stamping presses due to repetitive mechanical shock waves:
To ensure long-term survivability in heavy stamping environments, DeviceLab implements rigorous hardware hardening practices:
- Mechanical Damping & Silicone Encapsulation: Sensor conditioning printed circuit boards (PCBs) are potted with industrial polyurethane/silicone elastomer inside extruded aluminum enclosures, eliminating lead fatigue on electrolytic capacitors and inductors under continuous 20G shock pulses.
- Circular M12 Industrial Connectors: Traditional screw terminal blocks loosen under impact vibration. Sensor connections utilize IP67-rated M12 metallic circular screw-lock connectors with gold-plated pins.
- High-Frequency RC Noise Blanking: Stamping impacts cause mechanical relay contacts to bounce for 10ms–40ms upon stroke impact. Edge firmware executes a hardware-assisted blanking window, ignoring secondary oscillations occurring within 250ms of the initial stroke trigger.
3 Non-Invasive Signal Extraction Topologies for CNC Machining Centers
For CNC milling and turning centers, DeviceLab engineers capture high-fidelity production metrics without tapping into sensitive CNC controller motherboards:
1. 24VDC Andon Stack Light Signal Tapping
Connecting high-speed optocouplers across the three color tiers of the machine's external Andon light tower yields fundamental operational state data: Green (Automated Machining), Yellow (Manual JOG / Feed Hold / Setup), and Red (CNC Alarm / Axis Limit / Emergency Stop).
2. Capturing M02 / M30 Program Completion Relays
All Fanuc, Mitsubishi, and Siemens CNC controllers close an internal auxiliary dry-contact relay upon executing M02 (End of Program) or M30 (Program End & Rewind) G-code blocks. Monitoring this relay contact via an opto-isolated digital input increments the finished piece count with 100.0% precision, unaffected by intermediate tool changes or feed holds.
3. Spindle Motor Current Monitoring via Split-Core CT
By clamping a non-invasive current transformer around the main spindle inverter feed inside the electrical enclosure, the gateway samples real-time spindle motor current at 100Hz, enabling advanced load profiling.
Spindle Load Profiling: Separating Productive Cutting from "Air-Cuts"
A major source of hidden factory inefficiency occurs when CNC machines run "air-cuts"—the spindle is spinning and the G-code program executes, but the cutting tool is not engaging metal (e.g. excessive rapid traverse distances, operator dry runs, or forgotten workpiece blank loading):
Spindle Operating State Decomposition:
- State A: SPINDLE_OFF    --> I_spindle < 1.0A (Machine stopped or tool changing)
- State B: IDLE_SPINNING   --> 1.0A ≤ I_spindle ≤ 4.5A (Spindle rotating in air, zero cutting load)
- State C: ACTIVE_CUTTING  --> I_spindle > 4.5A (Cutter engaging workpiece metal)
- State D: TOOL_OVERLOAD   --> I_spindle > 14.0A (Excessive feed rate, dull tool, or imminent tool fracture)

True Cutting Efficiency Ratio (CER):
CER = Total_Active_Cutting_Time / Total_Program_Runtime
By isolating active cutting hours from idle spindle rotation, plant managers can optimize G-code toolpaths, compress rapid traverse delays, and detect tool wear before catastrophic tool breakage scraps expensive workpieces.
Bill of Quantities (BOQ): 20 Stamping Presses & 10 CNC Machining Centers
Below is an engineering cost estimate for digitizing a mixed fabrication shopfloor comprising 20 mechanical punch presses and 10 CNC machining centers:
| Item # | Hardware & Service Description | Qty | Unit Price (USD) | Total Amount (USD) | Engineering Deployment Role |
|---|---|---|---|---|---|
| 1 | DeviceLab DL-IOT-GW Heavy-Duty Edge Gateway (Dual isolated RS485, 4x DI, 4G/Ethernet) | 6 units | $95.00 | $570.00 | Each gateway monitors a cluster of 5 stamping presses or CNC machines. |
| 2 | 20G Shock-Hardened Stamping Sensor Conditioning Units (M12 connector, IP67) | 20 sets | $28.00 | $560.00 | Installed on punch press frames with hardware RC debounce filtering. |
| 3 | High-Speed Split-Core Current Transformers (50A/5A) for CNC spindle monitoring | 10 sets | $15.00 | $150.00 | Clamped on CNC spindle drive supply leads inside control panels. |
| 4 | Opto-Isolated 24VDC Andon & M-Code Interface Boards | 10 sets | $22.00 | $220.00 | Tapped into CNC machine Andon towers and M02/M30 completion contacts. |
| 5 | Industrial Belden Shielded Twisted-Pair Cabling, Conduit & Hardware Accessories | 450 meters | $1.15 / m | $517.50 | High-integrity noise-shielded cabling routed through overhead cable trays. |
| 6 | On-Site Installation, Machine Calibration, Noise Verification & Commissioning | 5 mandays | $120.00 | $600.00 | Physical panel integration, zero-interference verification, and dashboard setup. |
| TOTAL ESTIMATED TURNKEY PACKAGE (30 MACHINES): | $2,617.50 | Under $88 per machine (~2,200,000 VND / machine) for full shopfloor digitization. | |||
Field Problem Solving: 5 Machine Telemetry Issues and Resolutions
Review this troubleshooting matrix to resolve common physical layer signal anomalies on metalworking machines:
| Telemetry Fault Symptom | Electromechanical Root Cause | Oscilloscope / Telemetry Signature | Field Resolution Protocol |
|---|---|---|---|
| Ghost Part Counts on Mechanical Press | Crankshaft proximity sensor mounted too close to moving flywheel gear teeth; vibration trips sensor. | Double or triple pulses logged within a 150ms single-stroke window. | Readjust sensor mounting bracket air gap to 2.5mm; enforce 300ms software lockout in firmware. |
| CNC Program Count Increments During Tool Change | Operator used auxiliary M-code relay that fires during automatic tool changer (ATC) rotation. | Count increments 8 to 15 times during a single part setup cycle. | Rewire optocoupler tap strictly to the dedicated M02 or M30 program completion contact. |
| Spindle Load Data Corrupted with Random 999% Spikes | Current transformer secondary wires routed through wire duct parallel to high-voltage servo power leads. | PWM carrier frequency noise spikes (8kHz–16kHz) coupling onto analog input channels. | Reroute CT leads into separate low-voltage wire tray; twist secondary pair tightly; add 100nF bypass cap. |
| Andon Light Sensor Circuit Blown Out | Andon tower bulb burned out; replacement LED bulb wired with reverse polarity. | Optocoupler input diode reverse biased with zero conduction. | Incorporate bidirectional AC/DC optocouplers (such as PC814) that accept either voltage polarity. |
| Gateway Reboots Whenever Press Clutch Engages | Flywheel pneumatic clutch solenoid lacks flyback diode; high-voltage back-EMF couples onto 24VDC supply. | 24VDC power rail sags to 14V momentarily followed by a +85V inductive overshoot spike. | Install bidirectional TVS diode across clutch solenoid; power gateway from independent clean DC supply. |
5-Phase Turnkey Rollout Plan for 40-Machine Metalworking Plants
Executing factory telemetry without disrupting active production schedules follows a structured 5-phase methodology:
- Phase 1: Electromechanical Survey & Signal Mapping (Days 1–2): Catalog machine vintages, inspect electrical cabinet terminal strips, identify M-code relays, and measure ambient electrical noise.
- Phase 2: Single-Machine Benchmark Pilot (Days 3–5): Install prototype sensors on 1 press and 1 CNC; benchmark automated counts against manual caliper and piece tallies for 3 shifts.
- Phase 3: Cable Infrastructure & Overhead Tray Installation (Days 6–8): Pull shielded twisted-pair cables through overhead cable trays to all machine positions during weekend shifts.
- Phase 4: Clustered Machine Cutover & Hot Integration (Days 9–12): Install gateways, clamp CTs, and connect optocoupler taps machine-by-machine during scheduled tooling changeovers.
- Phase 5: Dashboard Commissioning & Operator Training (Days 13–14): Bind gateway MQTT streams to the central SCADA dashboard; train supervisors on real-time OEE reports.
Factory Case Study: 22% OEE Surge for Automotive Parts Plant at Khai Quang (Vinh Phuc)
An automotive stamping and precision machining supplier in Khai Quang Industrial Park (Vinh Phuc) operated 24 CNC vertical milling centers (Fanuc and Doosan) and 12 mechanical stamping presses (110T to 300T Komatsu). Plant management faced intense pressure from Tier-1 automotive assemblers to improve delivery predictability, but average plant OEE stagnated at 58.4% due to chronic untracked downtime between shifts.
The DeviceLab Engineering Team implemented a turnkey shopfloor telemetry deployment:
- Turnkey Hardware Instrumentation: Outfitted all 12 stamping presses with vibration-hardened stroke sensors and 24 CNC machines with spindle load current transformers and M30 completion taps. All data routed through 8 DeviceLab industrial gateways over plant Ethernet.
- Zero Disruption Rollout: The entire physical installation across 36 machines was completed in 10 working days without shutting down a single production line.
- Measured 10-Month Operational Results:
- Spindle Air-Cut Reduction: Spindle load telemetry revealed that CNC operators spent an average of 22 minutes per shift running air-cut dry runs due to overly conservative machining clearances. Optimizing toolpaths reduced cycle time by 9.4%.
- Downtime Visibility: Real-time automated dashboard alerts pinpointed that stamping presses spent 48 minutes per shift waiting for coil replenishment. Establishing a proactive material delivery staging protocol slashed waiting time by 75%.
- Overall OEE Achievement: Verified shopfloor OEE jumped from 58.4% to 80.4% (+22.0% absolute improvement), enabling the facility to increase monthly part shipments by $42,000 without capital investment in new machine tools.
Ready to capture real-time piece counts, spindle cutting loads, and OEE metrics from your CNC and stamping machinery? Contact the DeviceLab Automation Engineering Team via Hotline: (+84) 982.503.355 or submit your machine roster to hi@devicelab.vn for an on-site feasibility review and pilot PoC proposal within 24 hours.